Rotary Vane Pumps

Elmo Rietschle’s V-Series rotary vane pumps leverage decades of engineering expertise to deliver reliable, efficient, and versatile vacuum and compression solutions. Available in both oil-lubricated and dry running models, our pumps cater to diverse industrial needs while ensuring long up-time and minimal maintenance.


Oil-Lubricated Rotary Vane Pumps: 

Elmo Rietschle’s oil lubricated rotary vane pumps deliver reliable, consistent vacuum performance supported by long vane life, low noise output, and optimized oil circulation. This design ensures smooth operation under demanding conditions while maintaining proper internal lubrication and sealing. Select models in the V-Series are offered as oil lubricated rotary vane vacuum pumps or oil sealed rotary vane vacuum pumps for applications requiring deeper vacuum levels, enhanced vapor management, or superior internal sealing.


Dry Running Rotary Vane Pumps: 

Discover our dry running rotary vane pump solutions, engineered for oil-free performance in vacuum, pressure, and combination applications. Dry rotary vane vacuum pumps eliminate the risk of contamination associated with lubricated systems, offering clean, eco-friendly operation while maintaining outstanding durability and efficiency.


Oil-Lubricated Rotary Vane Pump Features

Extended Vane Lifespan: Our oil lubricated rotary vane pumps are engineered with durable materials and optimized lubrication paths, ensuring long vane life and reduced downtime.

Quiet Operation: Precision-balanced components and efficient airflow pathways help maintain quiet operation, even during demanding duty cycles.

User-Friendly Maintenance: A service-friendly design makes inspections and oil changes fast and straightforward, reducing overall maintenance requirements.

High Tolerance for Water Vapor: Systems configured as oil sealed rotary vane vacuum pumps deliver excellent handling of moisture-rich environments with enhanced vapor management.

Oxygen Handling Capabilities: Models approved for oxygen applications incorporate specialized features for safe handling.

XD-Version Pumps for Harsh Environments: For applications involving aggressive vapors or solvents, XD-rated versions of our oil lubricated rotary vane pumps provide reinforced protection and increased longevity.

Our oil-free rotary vane vacuum pumps offer eco-friendly solutions for clean, efficient vacuum applications. Features include:

  • Eco-Friendly Design: Operates without oil in the compression chamber, preventing contamination and reducing environmental waste.
  • Reliable, Safe Performance: Engineered to support stable operation in critical industrial processes.
  • Long Term Durability: Built with high-quality materials that minimize wear and extend equipment lifespan.
  • Simplified Upkeep: Straightforward access to service points ensures fast, hassle-free maintenance.
  • Low Noise Output: Designed for quiet operation in noise-sensitive environments.
  • Flexible Accessory Options: A variety of filters, valves, and configurations are available to customize performance.

Dry Running Rotary Vane Pump Features

Our dry-running oil-free rotary vane vacuum pumps offer eco-friendly solutions for clean, efficient vacuum applications. Features include:

  • Eco-Friendly Design: Operates without oil in the compression chamber, preventing contamination and reducing environmental waste.
  • Reliable, Safe Performance: Engineered to support stable operation in critical industrial processes.
  • Long Term Durability: Built with high-quality materials that minimize wear and extend equipment lifespan.
  • Simplified Upkeep: Straightforward access to service points ensures fast, hassle-free maintenance.
  • Low Noise Output: Designed for quiet operation in noise-sensitive environments.
  • Flexible Accessory Options: A variety of filters, valves, and configurations are available to customize performance.

Rotary Vane Vacuum Pump Performance & Technical Specifications

The V-Series rotary vane vacuum pump range is engineered for efficient vacuum generation, stable output, and reliable operation across a wide variety of industrial environments in the United States. Lubricated systems offer the strength and endurance of oil lubricated rotary vane pumps, while dry running pumps provide clean, oil-free solutions where contamination must be avoided.


Rotary Vane Vacuum Pump Performance and Technical Specifications

The Elmo Rietschle V-Series: Vacuum Pumps in Varying CFM Ranges

V-VTE

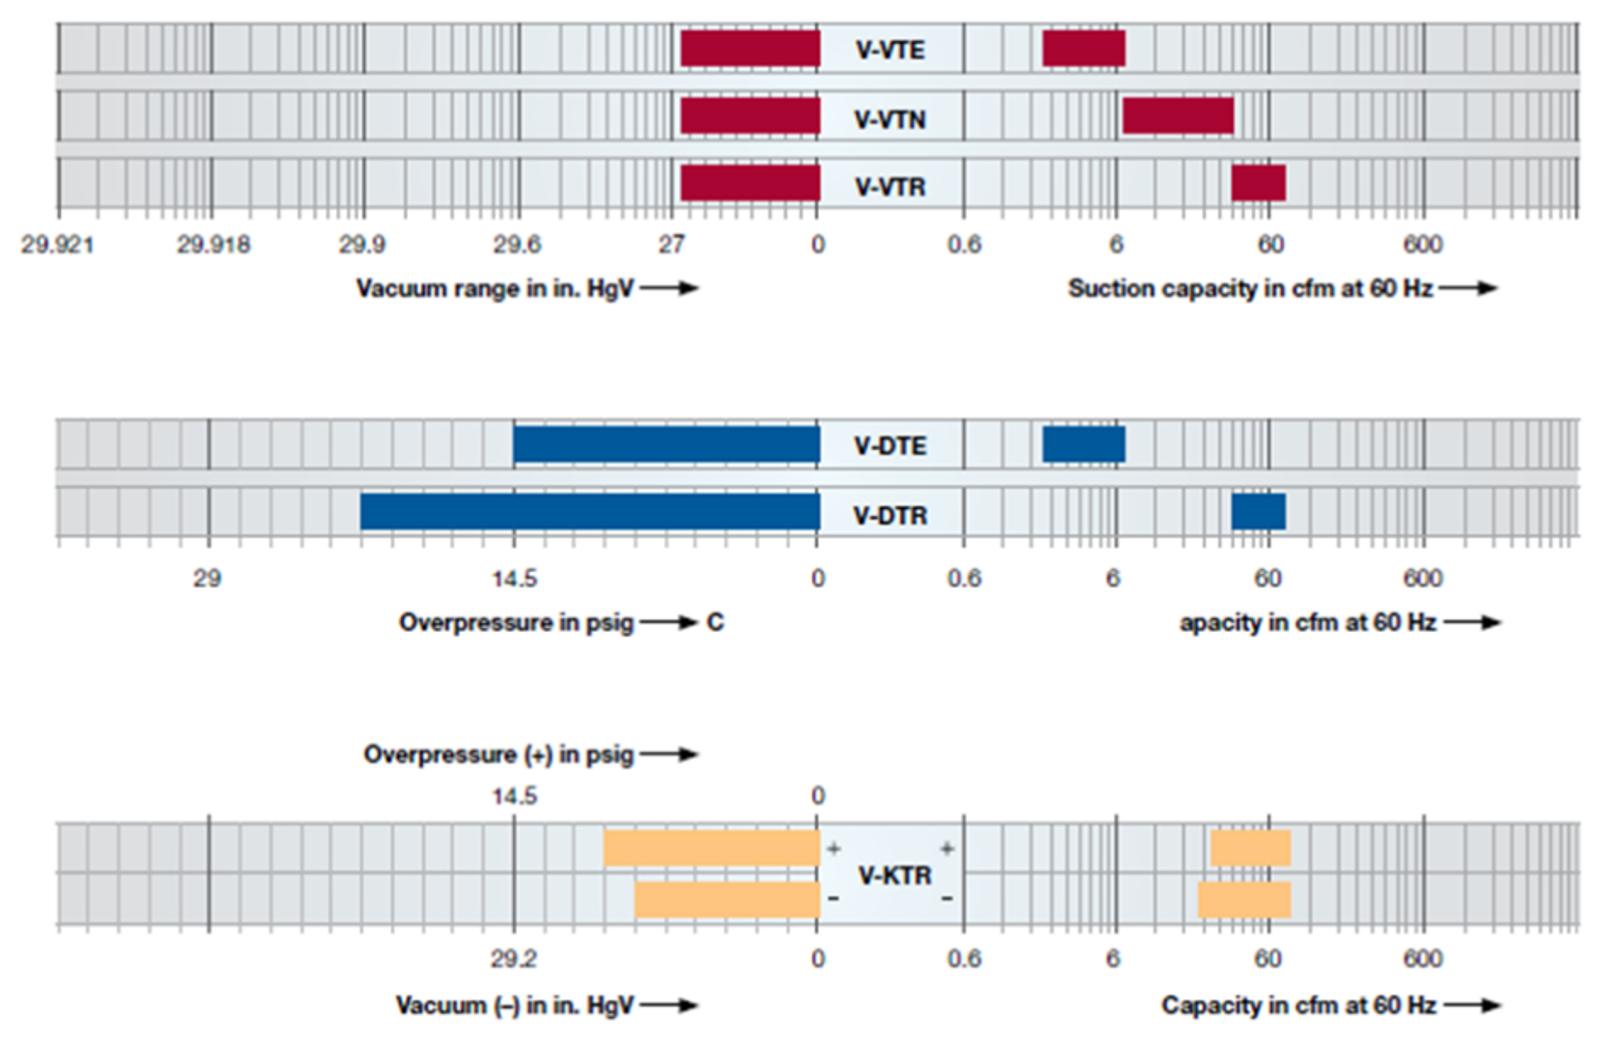
Capacities ranging from 2 to 7 cfm, ultimate vacuum 25.5 inHgV. Compact, easy to install. Low noise level and corrosion-resistant rotors, hose connection, and exhaust silencer as standard.

V-VTN

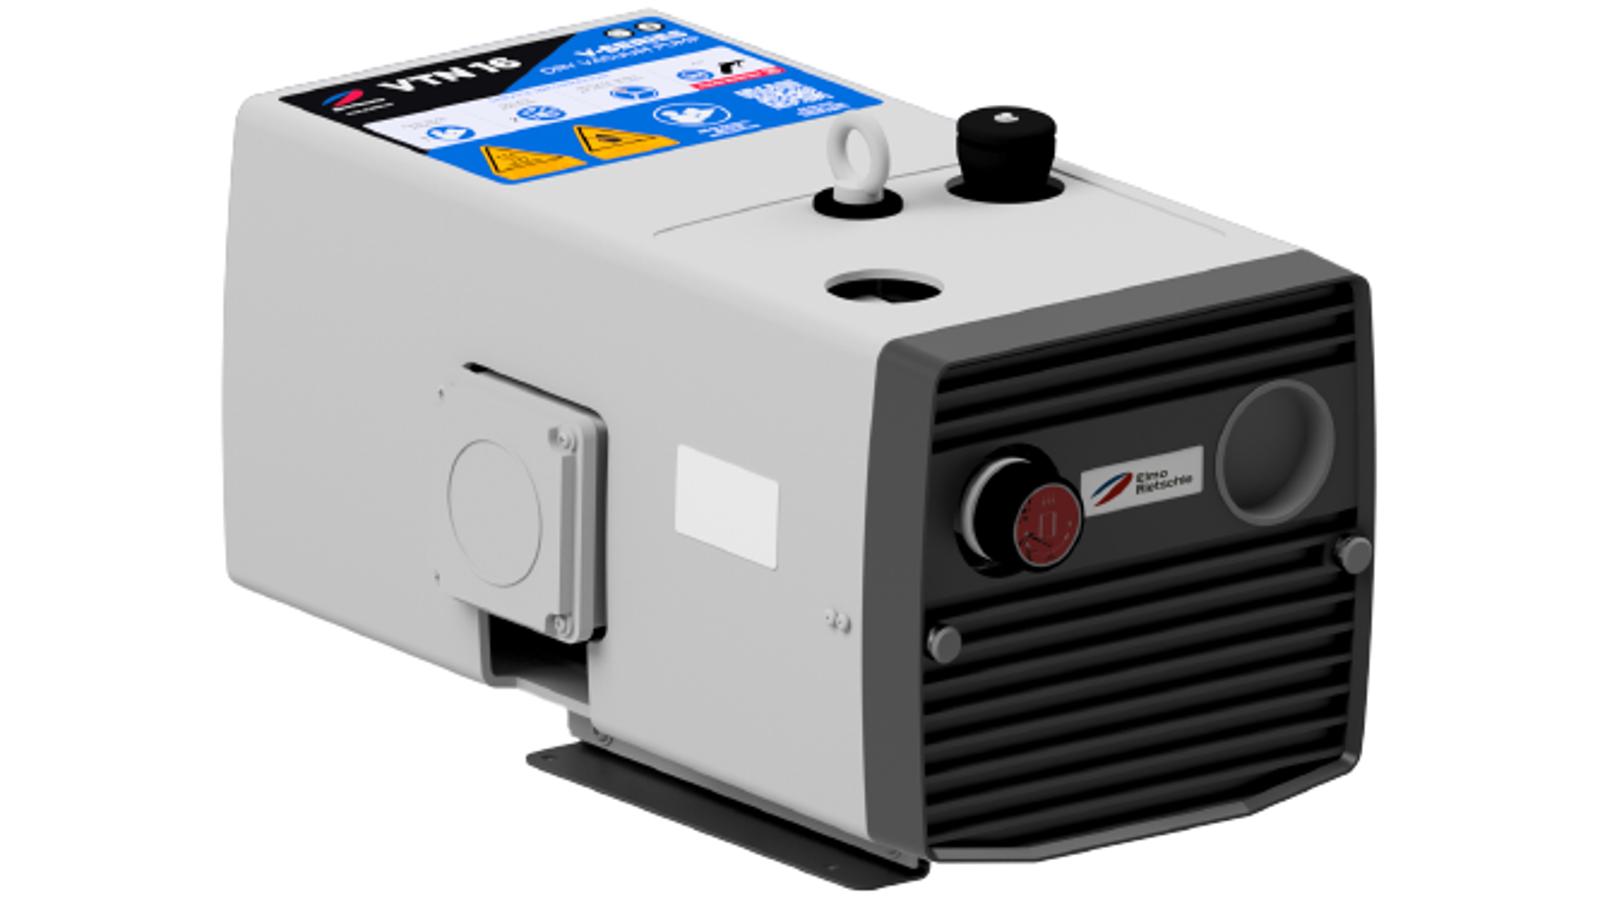
Capacities from 8 to 30 cfm, ultimate vacuum of 25.5 inHgV. Sound cover reduces noise level, enhances cooling and protects operators from touching hot surfaces. Comes with built-in suction filters and vacuum valves and low vibration, easy to operate, install and service.

V-VTR

Capacities from 39 to 91 cfm, ultimate vacuum of 25.5 inHgV. Featuring bearings on both sides of the rotor, and flange mounted motor with bolt coupling. High efficiency and low noise operation. Easy to operate and service.

V-DTE

Capacities from 2 to 7 cfm, pressure up to 14.5 psig. Compact design, easy to build into machines, with low noise level. Hose connector, inlet silencer and pressure relief valve fitted as standard.

V-DTR

Capacities from 36 to 91 cfm, pressure up to 22 psig for continuous operation and up to 32 psig for intermittent operation. Featuring bearings on both sides of the rotor, and flange mounted motor with bolt coupling. High efficiency and low noise operation. Easy to operate and service.

V-KTR

Capacities from 28 to 95 cfm, vacuum up to 18 inHgV, pressure up to 10 psig. High efficiency and low noise level. Sound cover allows a ducted cooling air outlet. Easy to operate and service.

V-VGD

Capacities from 6 to 11 cfm (10 to 24 m³/h), reaching an ultimate vacuum of up to 29.86 inHg (gauge) [2 mbar (abs.)]. This needs little space thanks to its overhung rotor design and integral motor. Standard models come with a fine mesh filter, vacuum non-return valve and oil separator. This pump is ideal for any environment as it is quiet running.

V-VCB

Capacities ranging from 12 to 16 cfm (20 to 26.5 m³/h), and an ultimate vacuum of 29.86 inHg (gauge) [2 mbar (abs.)]. Designed especially for installation into small vacuum packaging machines. Features a flange mounted motor, bearings on both sides of the rotor and air cooling. Fitted with a fine mesh filter, vacuum non-return valve and oil separator.

V-VCE

Capacities ranging from 15 to 29 cfm (25 to 30 m³/h); V-VCE at 29.62 inHg (gauge) [10 mbar (abs.)]; flange mounted motor, bearings on both sides of the rotor, air cooling. Fitted as standard with fine mesh filter, vacuum non-return valve, gas ballast valve and oil separator.

V-VC / V-VCS

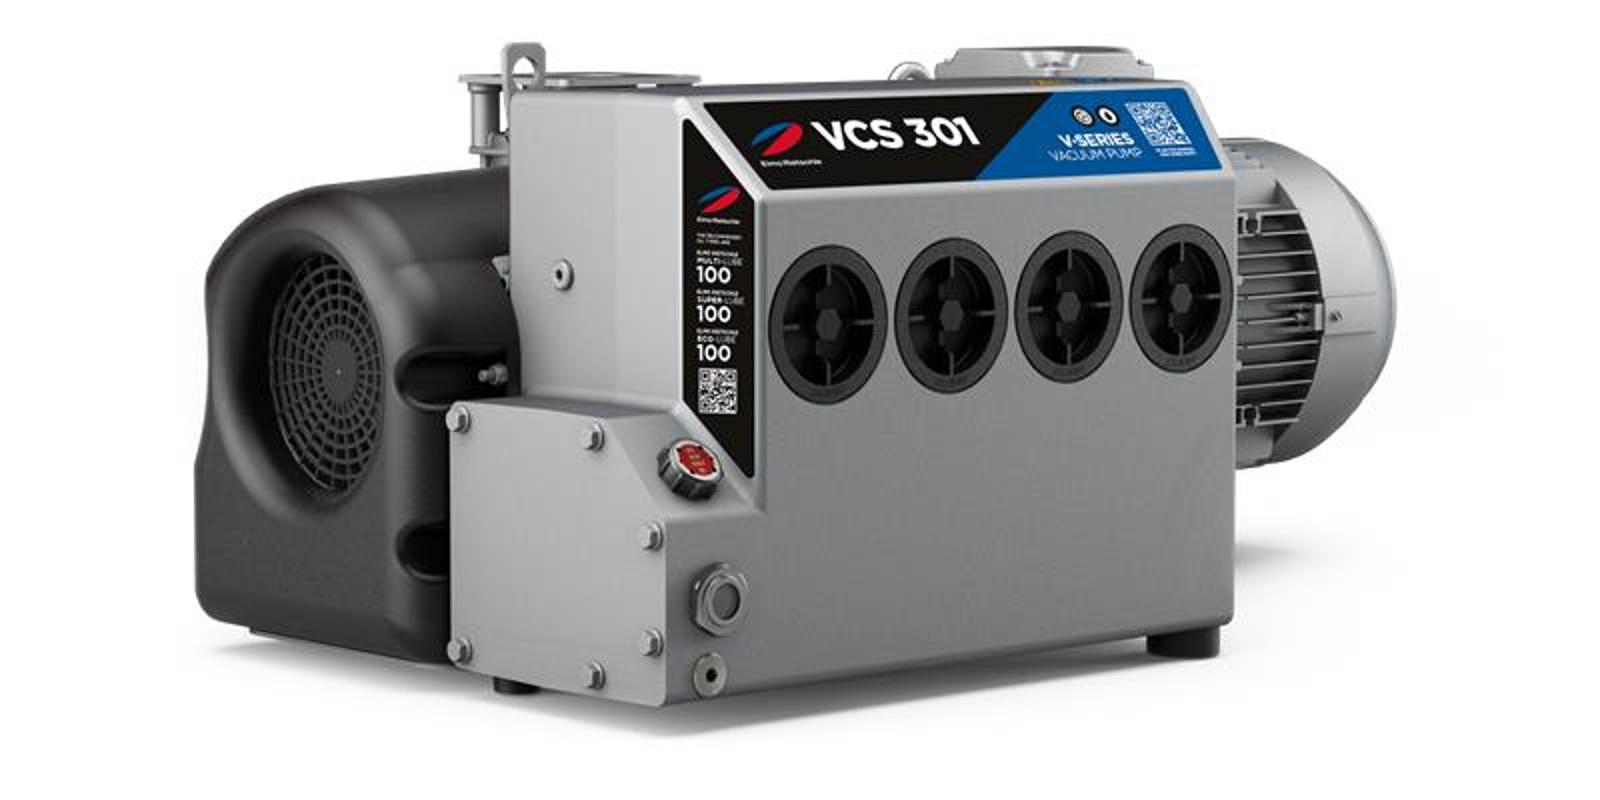
Capacities ranging from 30 to 903 cfm (40 to 1,535 m³/h), and an ultimate vacuum of 29.91 inHg (gauge) [0.5 mbar (abs.)]. Flange mounted motor, bearings on both sides of the rotor, oil/air heat exchanger. All models include aluminum alloy vanes, back pressure gauge, gas ballast valve(s), non-return valve and easy-access replaceable oil separators. Sizes of 400 m³/h and above include 5 micron paper inlet filter(s) and double-walled cylinder construction.
Innovating Industrial Efficiency with Rotary Vane Pumps

Elmo Rietschle’s engineered rotary vane systems support a wide range of industries across the United States. From stable vacuum generation to efficient compression, these pumps deliver energy-efficient, dependable performance that enhances uptime and supports critical production processes.

Oil-Lubricated Rotary Pump Applications

· Manufacturing environments requiring continuous-duty performance

· Packaging, forming, and material handling systems

· Industrial processes that depend on the durability of oil lubricated rotary vane pumps and the deeper vacuum performance available from oil lubricated rotary vane vacuum pumps


Dry Running Rotary Pump Applications

· Food processing and packaging

· Printing and woodworking

· Dust extraction and environmental engineering

· Drying and moisture-sensitive production environments

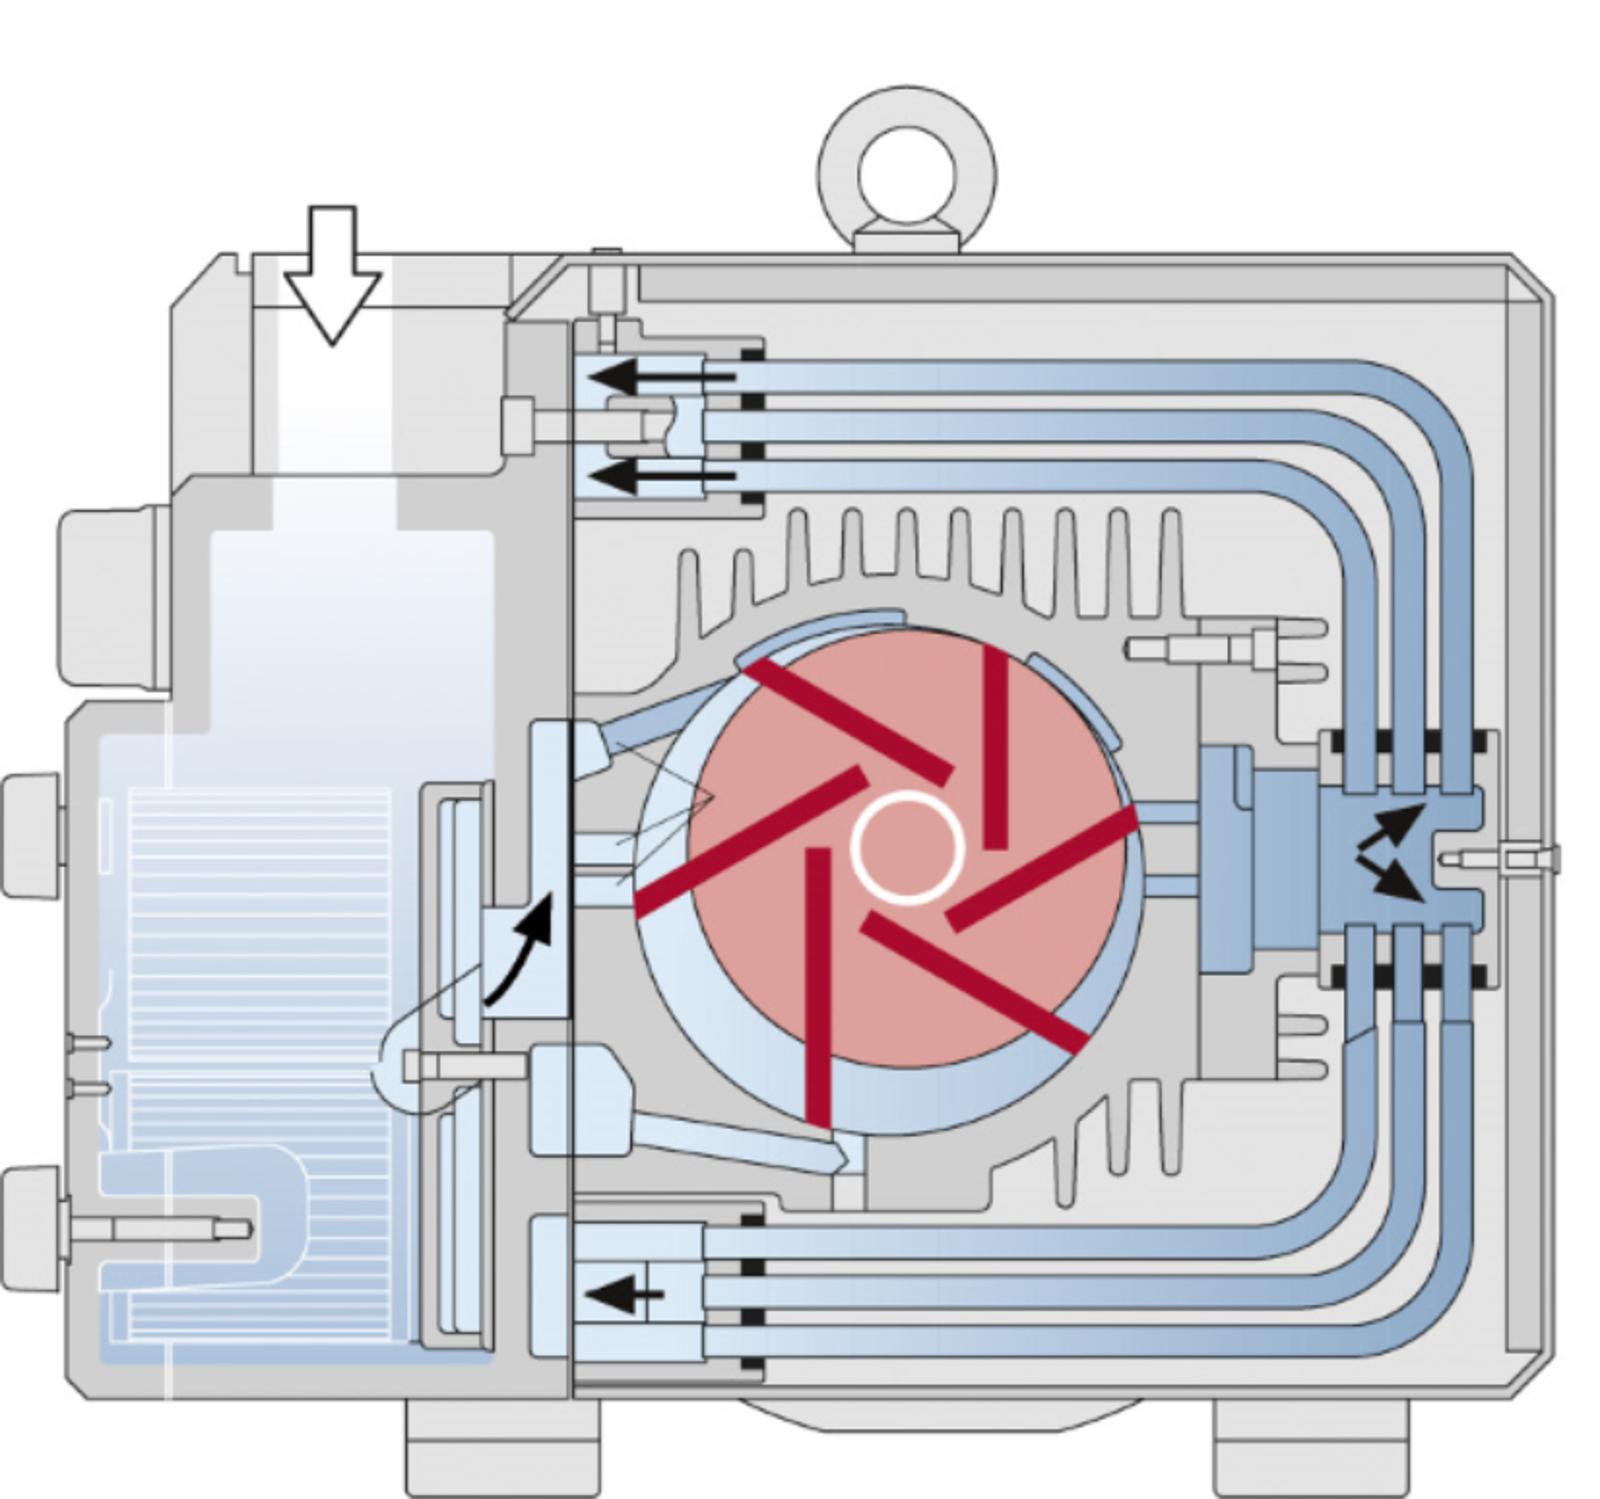
Both use the same rotor-and-vane operating principle. A rotary vane pump draws in and expels air to generate vacuum, while a rotary vane compressor uses the same mechanism in reverse to generate pressure. Elmo Rietschle’s V-Series dry running models, such as the V-DTE and V-DTR, are built specifically for pressure (compressor) duty, while the V-VTE, V-VTN, and V-VTR are built for vacuum duty. 
Dry Running Rotary Vane Vacuum Pump Operating Principle image

Discover the Technology Behind Reliable Compression

Explore more detailed product information about our Rotary Vane Vacuum Pump.